-
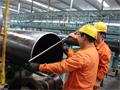
On November 28, the Singapore customers visited our company. Accompanied by Mr. Liu and Mr. Lu, customers visited the office and workshop. During the visit, Mr. Liu detailed introduced the producing process, working condition and the future plan of our company. The visit was in a relaxing and jovial atmosphere. Seeing the good condition of workshop and office, the customers gave a highly praise for our company.
-
Spiral pipe processing means on the basis of the original spiral pipe manufactured in accordance with the requirements of the requirements of the desired product.
There are two common spiral pipe processing methods.
First, the thermal expansion method
1. bulging law
One is placed in a rubber tube, with the upper punch compression, the tube shaped projection; Another method is forming a hydraulic bulging in the middle of the tube filled with liquid, the liquid pressure of the tube to the desired shape of the drum, bellows Most of the production is used in this method.
2. forging method
By swaging machine will be part of the red end of the tube or extension, reducing the outer diameter, commonly swaging machine has a rotary, link type, roller.
3. The bending method
There are three methods more commonly, a process called stretching method, another method called stamping method, a third roller method, a roller 3-4, two fixing rollers, a steering roller, fixing roller pitch adjustment, the finished tube It is curved.
4. stamping
In the punch with a core tapered end of the tube to expand to the required size and shape.
5. rolling method
Generally do mandrel, suitable for thick-walled tubes inside of the circle edge.
6. The roller method
The core is placed in the tube, with the outer periphery of the roller pushing for round edge processing.
Second, anti-corrosion method
Such steel is that people often say that the corrosion spiral steel pipe, this processing method is defined as the surface layer and the inner spiral pipe coated with a chemical coating, a common form of corrosion 3pe corrosion, anti-corrosion epoxy resin, cement mortar corrosion, such processing method biggest goal is to extend the life of the pipeline.
-
Pipe processing step requires strict, in which the hot rolling process is very important process, in which to introduce the following precautions during the heating pipe.
1, the pipe must be able to feed one of those metal properties were a good understanding Before rolling, when the deforming force is relatively low during the hot-rolled steel is very easy. But for the pipe material which still contains some ingot, so prior to hot rolling must be able to carry out some of them to eliminate those ingots, making it the organizational capacity and resilience are able to get some improvement, and also the pipe during the hot rolling process also will get a lot of protection.
2, be sure to pay attention to each pipe section has a temperature uniformity in all directions during the hot rolling process, so that the pipe can better meet the requirements of the various technological aspects in later. In addition, the heating pipe is will affect a very important reason for the life of the pipe.
3, on the pipe during the heating process in which there will be a lot less than expected occurrence of the accident, and therefore in the process of working among them must be taken to minimize the occurrence of these accidents.
4, for each indicator heating process and the technical requirements are able to do a comprehensive preparatory work, thus extending the life of the pipe.
5, the pipe in the heating process which will be very easy to cause oxidative phenomena pipe, thus there will be some for the original weight loss, so before heating must be able to take into account the reasons.
-
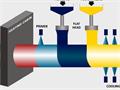
Cold-formed steel, cold-formed rectangular tube through the one-way roller contacts the outer tube forming the outer wall so that the strip bending moment, bending line will produce cold-formed compression, the compression effect makes bend lines longitudinally elongated, bent accumulation of the metal appears thicker, which is cold-formed compression / thickening effect.
1) The advantage of cold-formed is small rebound, forming accurate, and as long as the roller type accurately, inside corner molding R more accurate. The advantage is that it can be cold-formed side bent when you can not be cold-formed, for example, square and rectangular tube top / side synchronous bending and finishing. You can also cold-formed bent R <0.2t inside corners and walls without fracture.
2) There is a disadvantage of cold-formed stretching / thinning effects. It will produce cold-formed bends stretch, stretching effect of the longitudinal length of the bend lines shortened; second, cold bending of the metal due to stretching and thinning. The disadvantage is cold-formed in the top / side of sync when cold-formed, since the upper and lower rollers while generating pressure, easy molding force beyond the critical point, causing instability concave edge, and can also affect the stable operation of units and forming quality.
-
El método de moldeo para la fabricación de tubos de acero de sierra de gran diámetro es el método de moldeo UOE, una fila de método de formación de rollos (CFE), moldeo CE. Para la gran mayoría de los pasos finales del proceso de moldeo, se realiza una expansión del tubo posterior a la soldadura en toda su longitud, con el fin de mejorar la calidad de la forma del tubo de acero soldado. La expansión se convierte en una producción longitudinal de gran calibre para garantizar la calidad del tubo terminado, un proceso importante.
La expansión es un uso de medios hidráulicos o mecánicos para empujar la tubería de acero a lo largo de la pared de la tubería abombada radialmente hacia afuera en el proceso de moldeo por presión. Mecánico que en modo hidráulico, el dispositivo es simple y más eficiente, se adoptan varios procesos de sistemas de tuberías de diámetro ampliado longitudinales de gran calibre más avanzados del mundo, el proceso es el siguiente: Expansión mecánica del uso de la parte del lado dividido del diámetro ampliado de los segmentos se expanden radialmente, por lo que el tubo a lo largo de la dirección longitudinal de manera escalonada para lograr la longitud total de los segmentos del tubo del proceso de deformación plástica. Se divide en cinco etapas.
1. Círculo completo de la etapa inicial. Los segmentos se abren hasta que todos los segmentos están expuestos a la pared de la tubería, esta vez dentro del rango de pasos en varios puntos dentro del radio del tubo de acero son casi idénticos, círculo completo preliminar de acero.
2. El diámetro interior nominal del escenario. Los segmentos desde la posición frontal comenzaron a disminuir la velocidad, hasta llegar a la posición deseada, esta posición está dentro de los requisitos de calidad de la posición circunferencial de la tubería terminada.
3. Etapa de compensación del springback. Segmentos en posición para iniciar la segunda etapa más a baja velocidad hasta llegar a la posición deseada, esta posición está dentro de los requisitos de diseño del proceso complejo de misiles de la posición circunferencial de la tubería anterior.